Food & beverage
Sanitation that keeps working after the crew leaves.
From raw protein to bottling, Cognituv adds continuous treatment to surfaces, conveyors, cold rooms, process water and air, and puts the data next to your food-safety records.
 Case studyContinuous bio-security at 42,000 bottles an hourFood & beverage · Bottling plant · ArgentinaFood & beverageRead the case study
What’s at stake
The problems we hear most.
Re-exposure starts at restart
Sanitation resets the plant. Then product, people and air movement start re-exposing surfaces the moment the line runs again.
Cold, wet areas hold on to pathogens
Coolers, drains, drying rooms and condensate are where Listeria and other environmental pathogens tend to persist.
Chemical load adds up
Every extra sanitizer cycle costs labor and water and leaves residue to manage.
Auditors want records
FSMA, HACCP and customer audits all ask for the same thing: evidence.
Results from the field.
All case studies →Coca-Cola: Continuous bio-security at 42,000 bottles an hour
Food & beverage · Bottling plant · Argentina
A compact, high-fluence UV-C fixture built into existing machinery — continuous treatment on a 42,000 bph line, monitored through Connect.
Perdue Farms: Food safety with less acid on the line
Food & beverage · Poultry · Poultry processing line
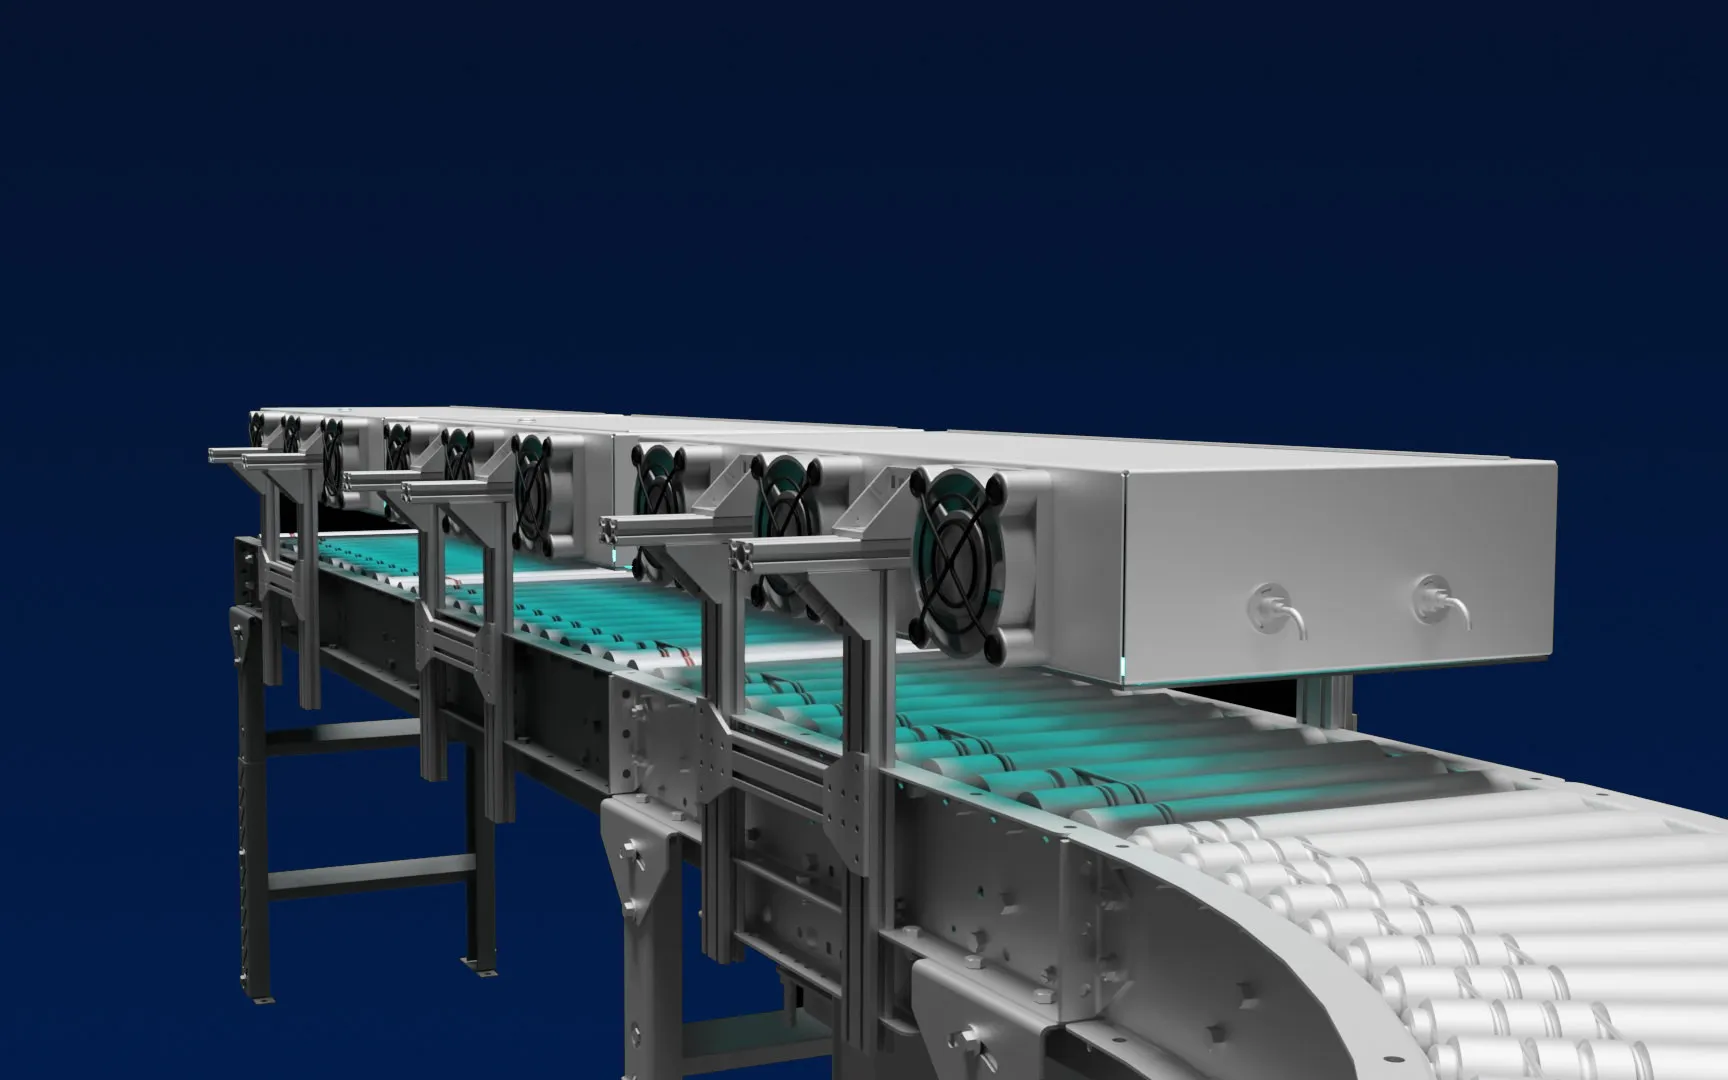
More peracetic acid was hurting workers and doing less against pathogens. A UV-C tunnel built into the conveyor line let the plant use less acid, with the dose monitored continuously.

Tuffy’s Pet Foods: Predictive maintenance on a 24/7 line
Food manufacturing · Perham, MN
Wireless vibration and temperature sensors on motors, conveyors and mixers — faults caught weeks before failure, with no wiring.
Where Cognituv fits
What we’d install, and where.
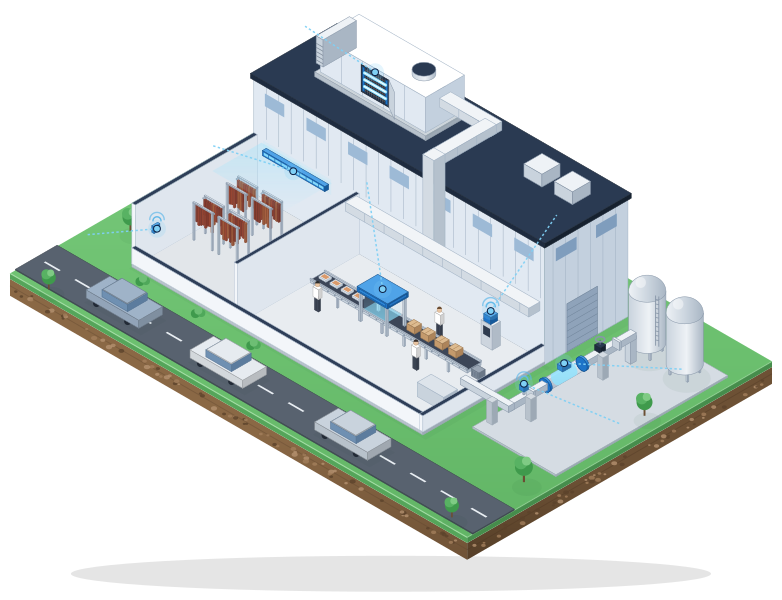
Point at a line, or tap it, to light its parts in the building.
Industrial UV-C
BARRICADE, MURAL, TUNNEL and ADAPT for surfaces, conveyors and drying rooms, and ICE for evaporator coils in coolers and freezers.
What you getTreatment keeps running between sanitation shifts, alongside your sanitation program and not in place of it.
See Industrial UV-CWater treatment
In-line UV-C for process and rinse water, with water-quality sensing.
What you getWater is treated as it flows, with fewer chemicals to buy, store, handle and document.
See Water treatmentCognituv Grid
On-coil UV-C for the air handlers that serve production and packaging.
What you getCleaner coils on the units that supply the line, with fewer chemical cleanings and less corrosive cleaner to handle near product.
See Cognituv GridCognituv Connect: UV-C record
UV-C run time, lamp status and output at the line, logged beside the rest of your food-safety data.
What you getOne record to hand an auditor. Lamps are changed on a schedule, or when the sensors show output has dropped.
See Cognituv ConnectCognituv Connect: room conditions
Temperature and humidity in drying rooms, coolers and cold storage.
What you getAn alert when a room drifts out of range, and the history that shows where it stayed the rest of the time.
See Cognituv ConnectCognituv Connect: water quality
pH, ORP and conductivity on process and rinse water, read continuously.
What you getYou know the water is in range between lab samples, with alerts on excursions.
See Cognituv Connect
Facility types
What changes from one facility type to the next.
What we look at first, where Cognituv fits and what you get from each item, the systems we usually find and the codes and standards to check. Codes and standards are listed for reference: a listing isn’t a compliance finding, and doesn’t mean any product, Cognituv’s included, is certified to one.
Food processing plant
Raw and ready-to-eat production, from cutting rooms and cook lines to packaging, with storage on site.
Includes: Meat and poultry processing · Dairy processing · Produce processing · Packaged-food manufacturing
- We look at
- Surfaces and conveyors between sanitation cycles
- Evaporator coils and drain pans in cold rooms
- Records an auditor can read
Where Cognituv fits and what you get
- Industrial UV-C: BARRICADESurface treatment that keeps running between sanitation shifts, alongside your program and not in place of it.
- Industrial UV-C: TUNNELTreats product and packaging on the conveyor, with the dose held as line speed changes.
- Industrial UV-C: ICETreats evaporator coils in coolers and freezers in place, at cold-room temperatures.
- Water treatmentProcess and rinse water treated as it flows, with fewer chemicals to buy, store and document.
- Cognituv GridCleaner coils on the air handlers that supply the line, with less corrosive cleaner used near product.
- Cognituv Connect: UV-C recordRun time, lamp status and output logged beside your food-safety data, ready for the auditor.
- Typical systems
- Evaporator coils · Air handlers · Rooftop units · Refrigeration systems
- Codes and standards
- IBC groups to screen
- F-1 (Factory: moderate hazard) · S-1 (Storage: moderate hazard) · S-2 (Storage: low hazard) · B (Business)
Beverage and bottling plant
Filling, capping and packaging lines with process water, CIP and syrup handling.
Includes: Bottling plant · Brewery · Winery
- We look at
- Filling and capping areas
- Process and rinse water
- Tanks, coolers and the air handlers serving them
Where Cognituv fits and what you get
- Industrial UV-C: ADAPTFixtures over the filling and capping line add treatment between sanitation cycles.
- Water treatmentRinse and process water treated in the pipe, with fewer chemicals to buy, store and document.
- Cognituv GridCleaner coils on the air handlers serving the filling room, with fewer chemical cleanings.
- Cognituv Connect: water qualitypH, ORP and conductivity between lab samples, with an alert when rinse water drifts.
- Cognituv Connect: UV-C recordLamps are changed on a schedule, or when Connect’s UV-C sensors show output has dropped.
- Cognituv Connect: tank and cooler temperatureTime-stamped temperatures, so an excursion and its recovery are both on the record.
- Typical systems
- Air handlers · Refrigeration · Process cooling · Process and rinse water
- Codes and standards
- IBC groups to screen
- F-1 (Factory: moderate hazard) · F-2 (Factory: low hazard) · S-1 (Storage: moderate hazard) · S-2 (Storage: low hazard) · A-2 (Assembly: dining, drinking and casino gaming)
Refrigerated and frozen warehouse
Chilled and frozen warehouses, where every door opening brings warm, humid air onto the evaporator coils.
Includes: Cold storage warehouse · Frozen-goods warehouse · Cold-chain distribution
- We look at
- Evaporator coils and drain pans
- Temperature and door-open time
- Humidity where condensation appears
Where Cognituv fits and what you get
- Industrial UV-C: ICETreats evaporator coils in place at freezer temperatures, in rooms that are costly to warm up and wash down.
- Industrial UV-C: BARRICADECeiling, wall or mobile-cart fixtures treat surfaces in coolers and staging areas between washdowns.
- Cognituv Connect: room temperatureTime-stamped temperatures by room, so an excursion and its recovery are both on the record.
- Cognituv Connect: door-open timeShows how long each door stood open, beside the room’s temperature.
- Cognituv Connect: humidityTemperature and humidity where condensation appears, so you can see what sets it off.
- Cognituv Connect: vibrationTrends and alerts on compressors and condenser fans, so the repair lands in a planned window.
- Typical systems
- Evaporator coils · Industrial refrigeration · Ammonia systems
- Codes and standards
- IBC groups to screen
- S-1 (Storage: moderate hazard) · S-2 (Storage: low hazard) · H (High hazard)
Indoor farm and greenhouse
Controlled-environment crop production, where heat, humidity and disease pressure set the operating plan.
Includes: Indoor vertical farm · Production greenhouse
- We look at
- Grow beds and crop surfaces
- Heat and humidity at the canopy
- The air handling that serves the grow rooms
Where Cognituv fits and what you get
- Industrial UV-C: GROWTreatment at the grow bed, with a reflector designed to spread the dose evenly across it.
- Cognituv GridCleaner coils on the units that cool and dry the grow rooms, with fewer shutdowns mid-crop.
- Water treatmentIrrigation and wash water treated as it flows, with fewer chemicals to buy, store and handle.
- Cognituv Connect: canopy climateTemperature and humidity at the canopy, room by room, with an alert when one drifts.
- Cognituv Connect: lightShows whether each bench gets the daily light its plants need.
- Typical systems
- Precision air handlers · Dehumidification · Supplemental cooling
- Codes and standards
- IBC groups to screen
- F (Factory and industrial) · U (Utility and miscellaneous) · M (Mercantile)
By segment
The method is the same across the plant floor. Where the risk sits, and where UV-C fits, changes by product.
Meats
Cutting rooms, conveyors and coolers carry the most risk. Surface UV-C over belts and tables, and indirect units in curing and drying rooms, add treatment between washdowns.
Poultry
High water use and fast lines make process water and conveyors the priority, with cold-coil UV-C in chill areas.
Seafood
Constant moisture and short shelf life put the focus on rinse water, ice and cold storage.
Dairy
Process water and filling and packaging areas come first, plus the air handlers serving them.
Cheese
Aging rooms need airborne mold under control without disturbing the cultures you want. Indirect room UV-C and on-coil treatment keep the room’s air handling clean.
Ready-to-eat meals
With no kill step after packaging, post-cook handling, slicing and packaging surfaces matter most.
Frozen foods and ice cream
Freezer and cooler coils, condensate and packaging lines. ICE fixtures are rated for sub-zero rooms.
Cold storage and distribution
Evaporator coils and drain pans in coolers grow biofilm that ends up in the room air. Cold-coil UV-C treats them in place, and Connect logs temperature and humidity.
Leafy greens
Wash water and conveyors handle product that is often eaten raw, so wash-water UV-C and belt treatment add a layer.
Vegetables and potatoes
Storage humidity drives mold and rot. Room air treatment and rinse-water UV-C support longer storage.
Fruit
Packing-house conveyors, storage rooms and wash water are the control points.
Bakery
Mold spores in cooling and packaging areas shorten shelf life. Room UV-C over cooling conveyors and packaging is the usual starting point.
Confectionery
Sugar, moisture and handling invite mold and yeast in packaging. Surface UV-C on packaging lines adds treatment without chemical residue on product.
Snacks, cereal and seeds
Low-moisture foods can still carry Salmonella, so dry-sanitation areas and conveyors benefit from treatment that adds no water.
Spices and seasonings
Dry handling and blending areas need treatment that adds no moisture. UV-C over conveyors and packaging fits that.
Sauces and condiments
Process water, tank surroundings and filling lines are the control points.
Sugars and syrups
Bulk storage and process water can carry yeast and mold. In-line UV-C on water and treatment around tanks and filling help.
Identify · Apply · Verify™
How a project runs.
Identify
We map the risk with your QA team: surfaces, conveyors, cold rooms, process water and the air handlers serving them.
Apply
UV-C sized to each surface and schedule, installed around production.
Verify
Run time, UV-C output, temperature and water quality report into Cognituv Connect, and your environmental monitoring program shows the result.
Where we work: Meat, poultry and seafood, Dairy and cheese, Bakery and confectionery, Produce and fresh-cut, Beverage and bottling and Cold storage and distribution.
Codes and standards
The references to check, each linked to its publisher.
The list comes from Cognituv’s facility and code library, reviewed September 2026. Publication isn’t adoption: whether a document applies, and which edition, depends on your jurisdiction, its amendments and your project, and the authority having jurisdiction decides. A listing isn’t a compliance finding for your facility, and doesn’t mean any product, Cognituv’s included, is certified to it.
FSMA, 21 CFR 117Federal statute
FDA Food Safety Modernization Act; Preventive Controls for Human Food, 21 CFR Part 117
Risk-based food-safety law, applied through rules for each activity; Part 117 covers preventive controls for human food.
Listed for: Food processing plant, Beverage and bottling plant, Refrigerated and frozen warehouse
HACCPFramework
Hazard Analysis and Critical Control Point (HACCP)
Hazard analysis with documented critical control points; the rule that applies depends on the food and the agency.
Listed for: Food processing plant, Beverage and bottling plant, Refrigerated and frozen warehouse
SQF CodeCertification program · Editions 9 and 10
Safe Quality Food (SQF) Code
Food safety and quality certification, audited against the code for your sector.
Listed for: Food processing plant, Beverage and bottling plant
OSHA 29 CFR 1910Federal regulation
Occupational Safety and Health Standards for General Industry, 29 CFR Part 1910
Workplace safety rules for general industry; which sections apply depends on the hazards and work on site.
Listed for: Food processing plant, Refrigerated and frozen warehouse, Indoor farm and greenhouse
FSMA Produce Safety, 21 CFR 112Federal regulation
Standards for the Growing, Harvesting, Packing, and Holding of Produce for Human Consumption, 21 CFR Part 112
The FSMA Produce Safety Rule: minimum standards for farms that grow, harvest, pack or hold covered produce, including worker hygiene, agricultural water and records.
Listed for: Indoor farm and greenhouse
See what the data says about your facility.
Start with a no-cost assessment: a call with an engineer and a written recommendation. When you want the data first, Cognituv Connect measures your own equipment, scoped and quoted for your site.
Prefer to talk? Call 1-888-580-8738